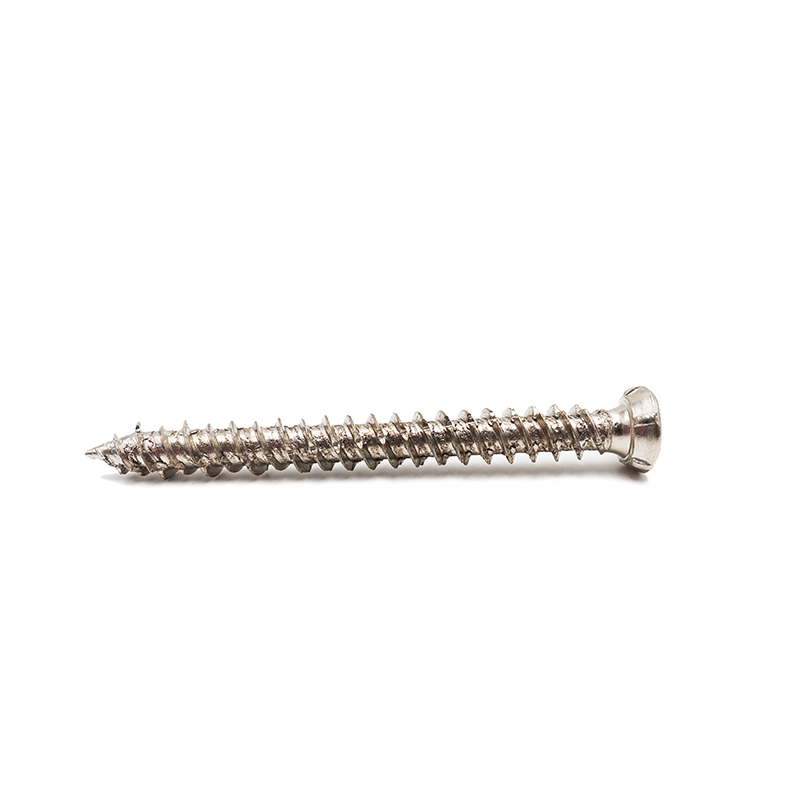
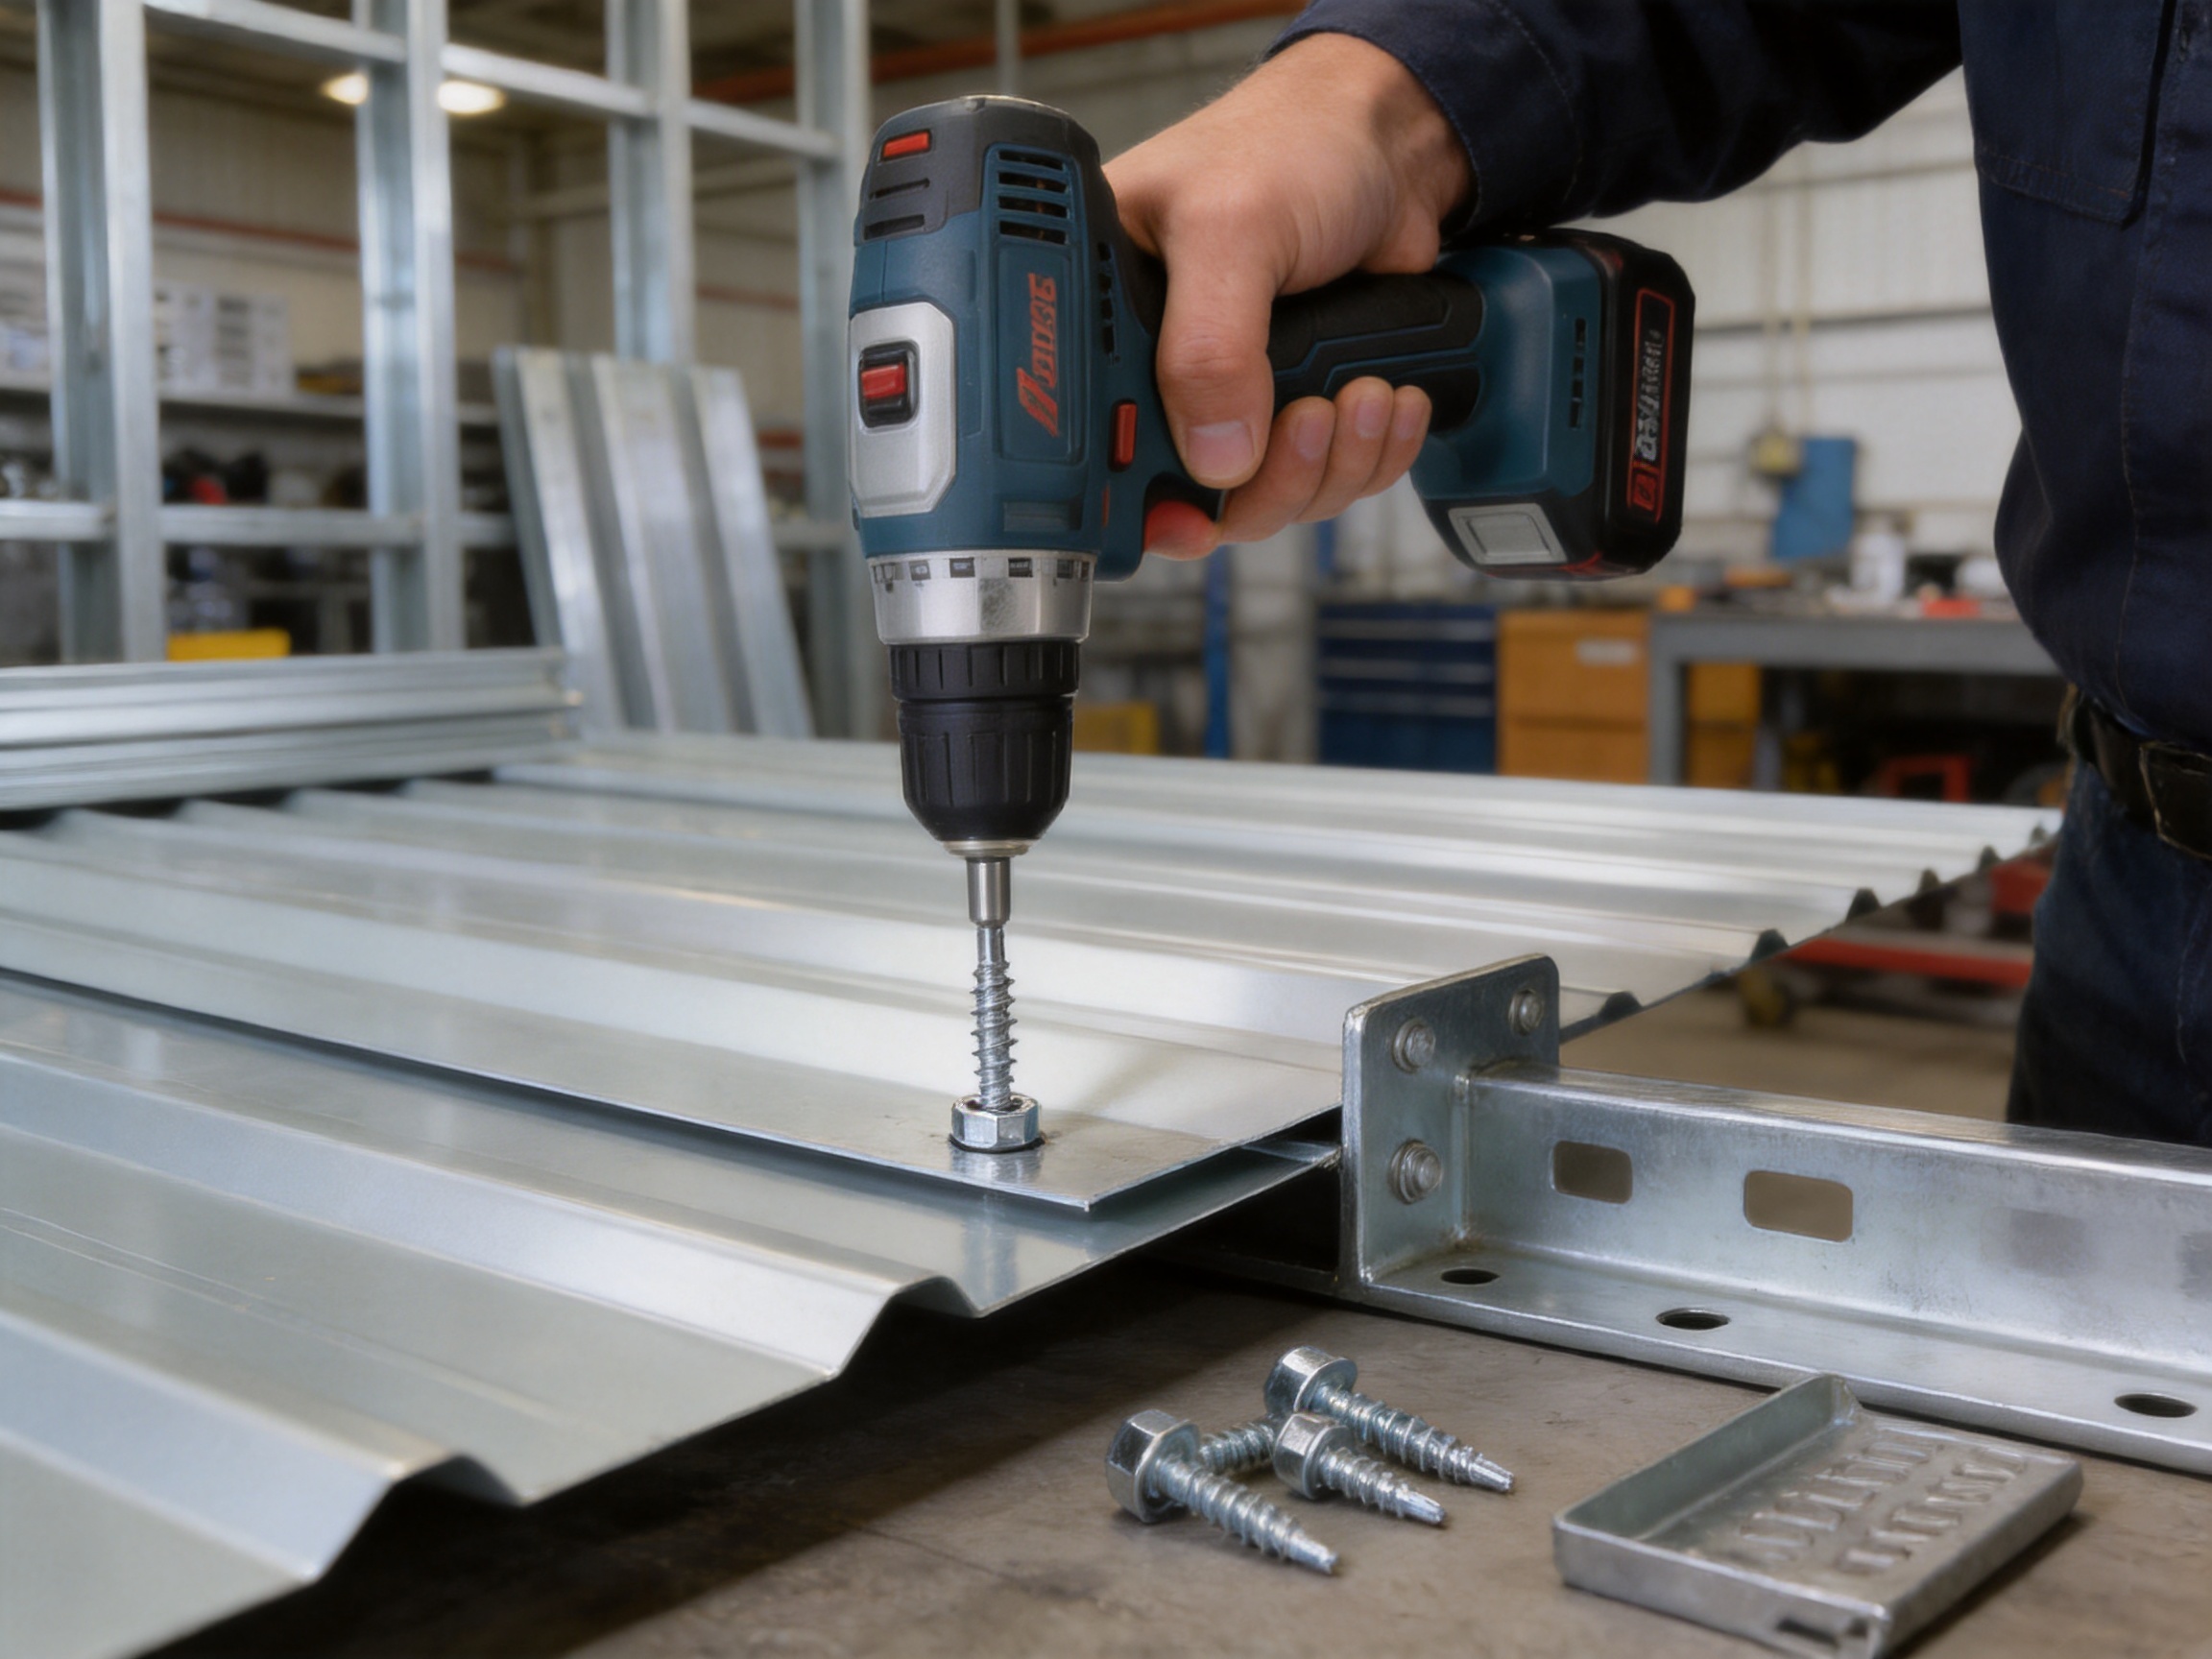
Hex washer head self-drilling screws are designed for fast, efficient, and dependable fastening in metal, construction, home improvement, furniture, packaging, and general hardware applications. By combining a drilling point, a hexagonal driving head, and an integrated washer flange, this screw design helps installers create a secure connection without the need for a separate pilot hole or loose washer.
The zinc-plated self-drilling screw described in this article is manufactured for users who need a practical balance of drilling performance, holding strength, corrosion resistance, installation speed, and dimensional consistency. It is produced from C1022A carbon steel and is available in several diameters, head styles, recess options, surface treatments, and thread configurations. This range allows distributors, contractors, manufacturers, and professional users to select a suitable fastener for different substrates and working conditions.
Compared with ordinary sheet metal screws, standard machine screws, or separate bolt-and-washer assemblies, a hex washer head self-drilling screw can simplify installation and reduce the number of components required. Its integrated washer head distributes pressure over a broader area, while the drill point is shaped to penetrate thin and medium-gauge metal more efficiently. When matched with the correct length, diameter, driver, and application, the fastener can support clean production work and consistent field installation.
Product Overview
The product is a zinc-plated hex washer head self-drilling screw intended primarily for fastening metal components. It may also be selected for certain construction, roofing, home tool, furniture, packaging, and fabrication applications where the base material and load requirements are suitable.
The main product characteristics include a hex washer head, self-drilling point, C1022A material, zinc-plated surface, and availability under commonly used self-drilling screw standards. The production range also includes other head types, recesses, diameters, and finishes, allowing the same manufacturing program to serve multiple customer specifications.
| Item | Available Specification or Feature | Practical Benefit |
|---|---|---|
| Product type | Hex washer head self-drilling screw | Fast drilling and secure clamping with an integrated flange |
| Material | C1022A carbon steel | Suitable strength and formability for general screw production |
| Diameter range | #6-3.5, #8-4.2, #10-4.8, #12-5.5, #14-6.3 | Selection for different material thicknesses and fastening loads |
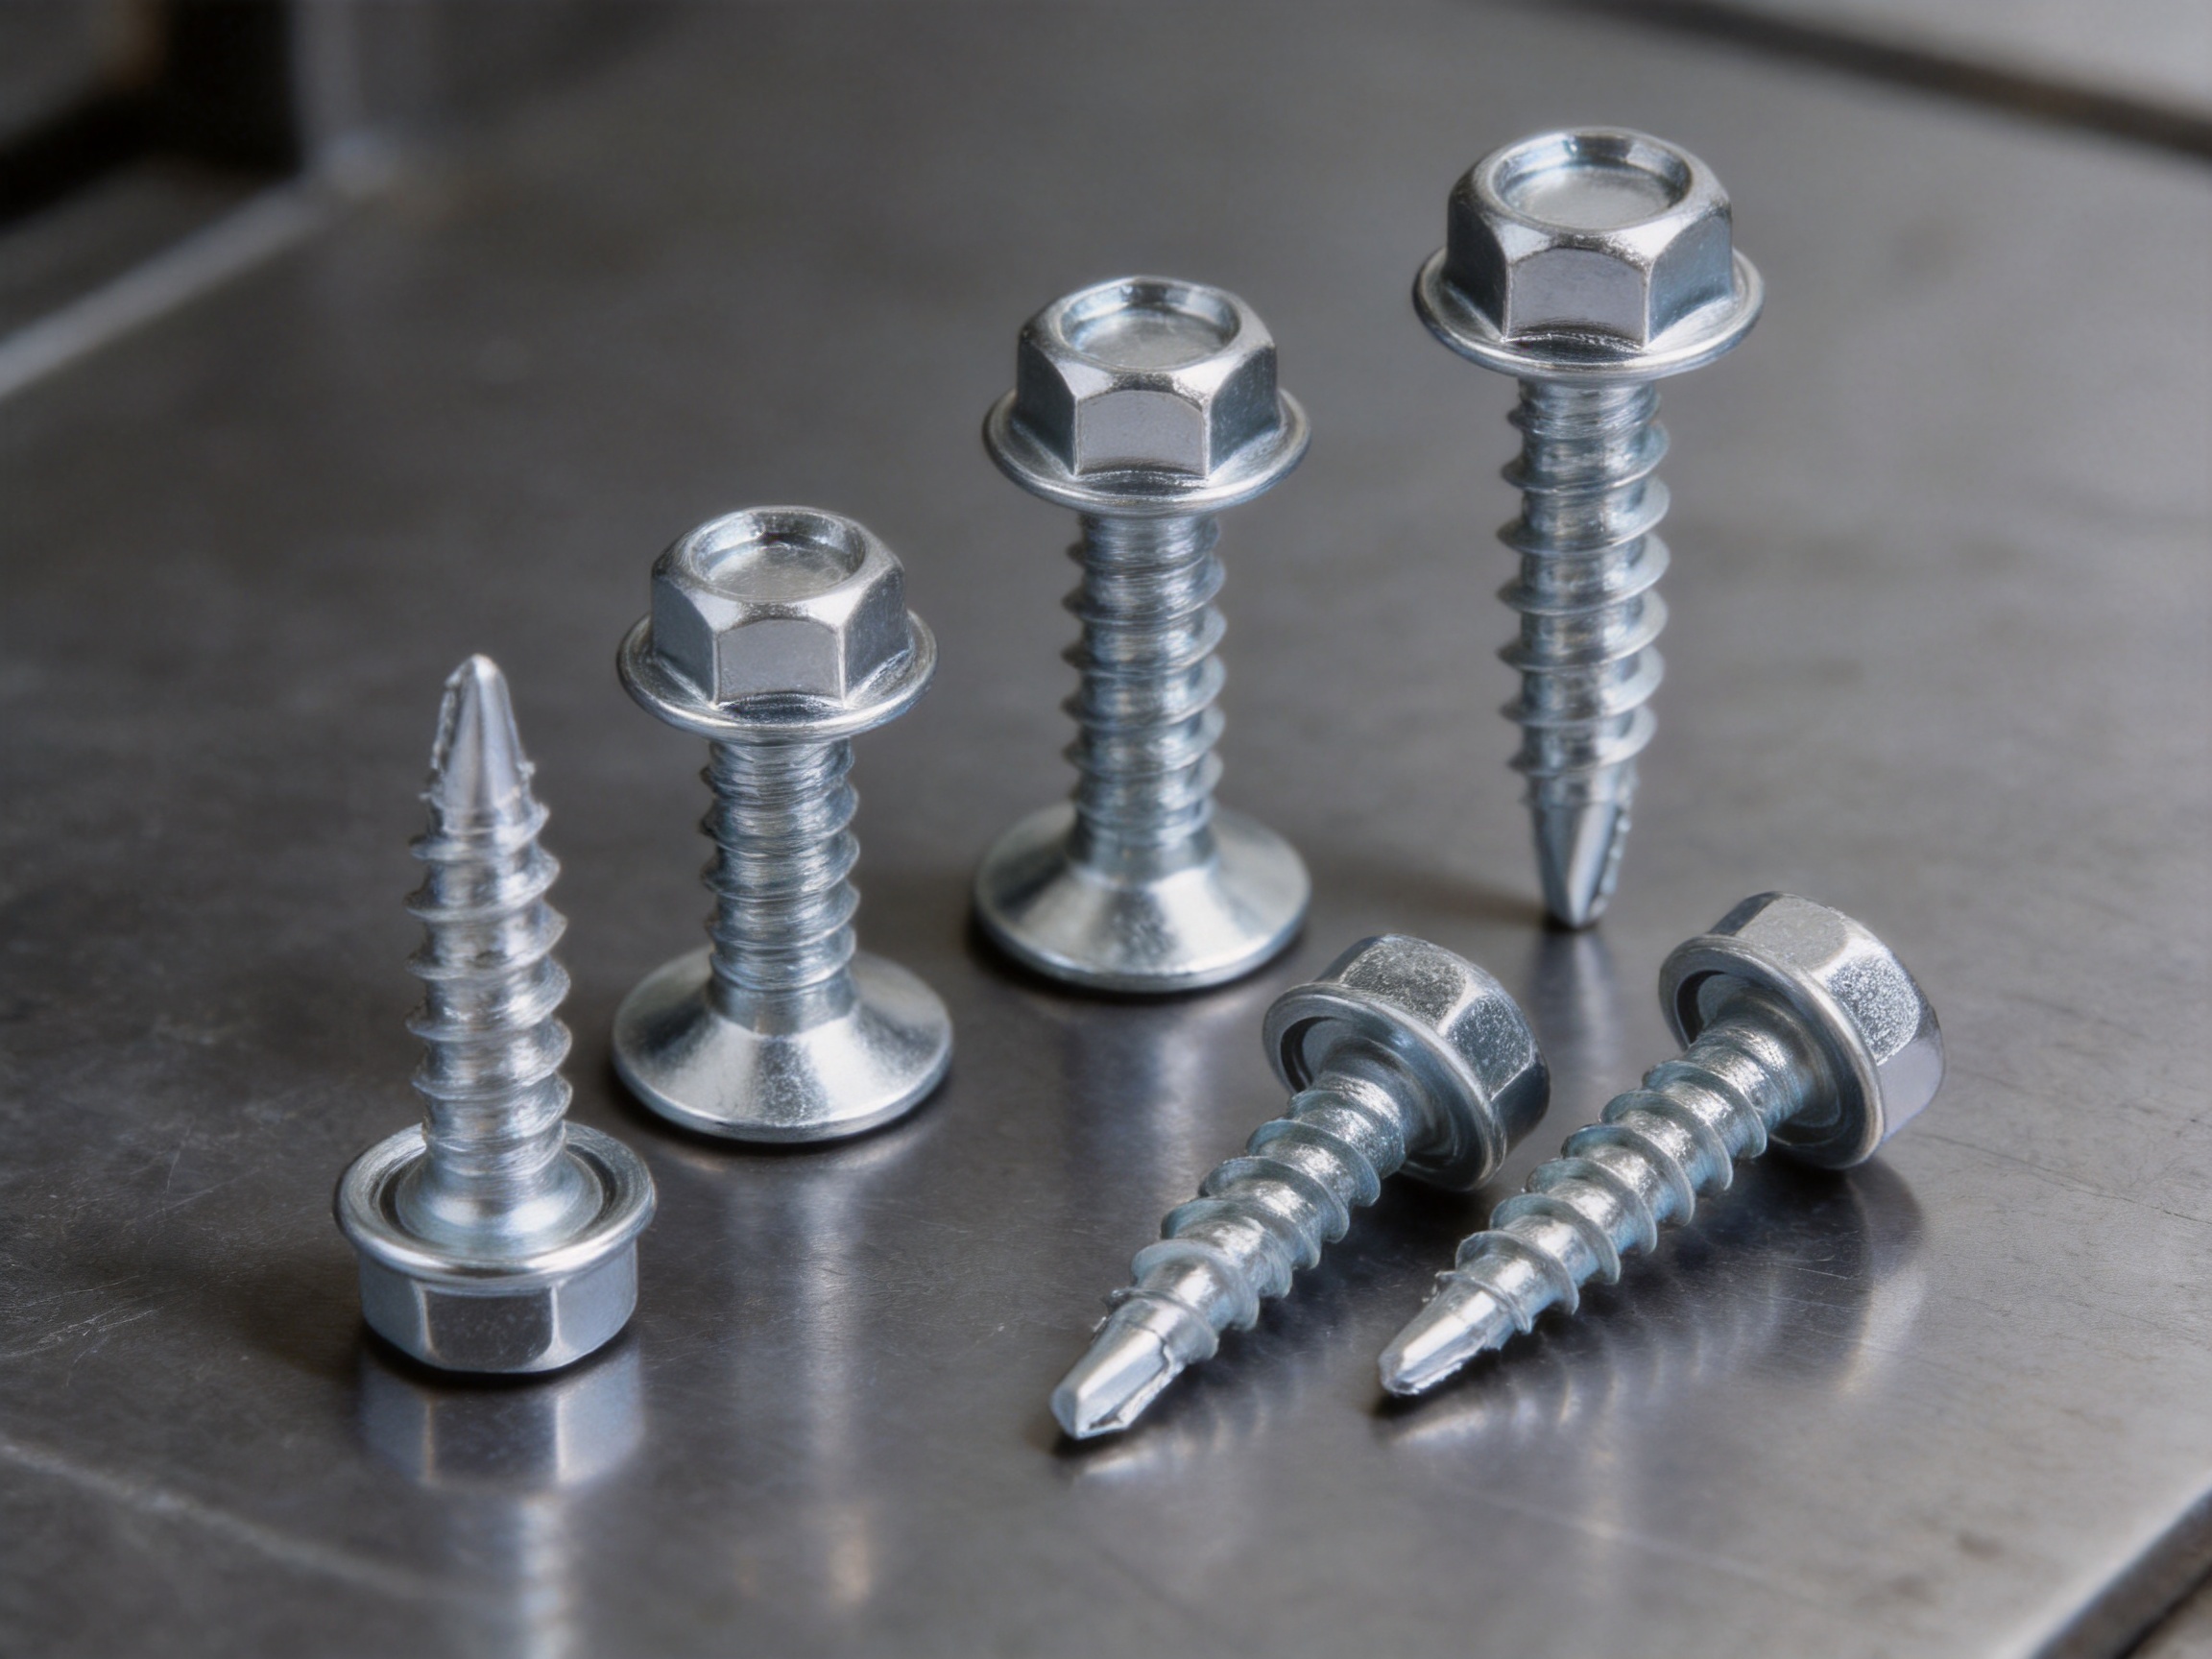
| Head options | Hex washer, bugle, flat, pan, wafer, and pan framing head | Adaptation to different assemblies and installation tools |
| Recess options | Phillips, square, and Torx | Choice of driving system and torque transmission |
| Thread options | BSD thread and CSD thread | Adaptation to different drilling and fastening requirements |
| Surface options | Zinc plated, yellow zinc plated, black phosphate, Ruspert, and Magni | Different levels of appearance and environmental protection |
| Referenced norms | ASTM, DIN 7504K, DIN 7504P, and DIN 7504N | Support for specification-based purchasing and application selection |
The broad specification range is important for wholesalers and industrial buyers. Instead of sourcing each screw type from a different supplier, customers can evaluate several related products through one production program. This may simplify purchasing, packaging, inventory planning, and private-label development.
How the Hex Washer Head Design Improves Fastening
The hex washer head is one of the most functional features of this screw. A hexagonal outer profile can be driven with a socket or nut driver, allowing the installer to apply torque directly through the six-sided head. This is particularly useful in applications where a Phillips or square recess may not provide enough driving control, or where the screw must be installed quickly with a power tool.
The washer flange is formed as part of the head rather than supplied as a separate component. During tightening, this flange bears against the surface of the material and helps distribute the clamping force. The wider bearing area can reduce the likelihood of the head pulling through thin sheet material when the fastener is properly selected and installed.
An integrated washer also supports production efficiency. A separate loose washer requires an additional handling step, may fall off during assembly, and creates another inventory item. The washer head keeps the fastening components together, making the screw easier to feed, carry, position, and install.
In metal fabrication, the hex washer head can be especially valuable when the installer needs stable tool engagement. The outer hex profile provides a visible and positive driving interface. This can help reduce wasted time caused by repeated bit repositioning, although the correct socket size and controlled installation torque remain essential.
The head geometry must be considered together with the thickness and hardness of the fastened material. A large flange may be beneficial for surface coverage, while a smaller head may be preferred where clearance is limited. The available head styles allow the buyer to choose a suitable design rather than treating every fastening task in the same way.
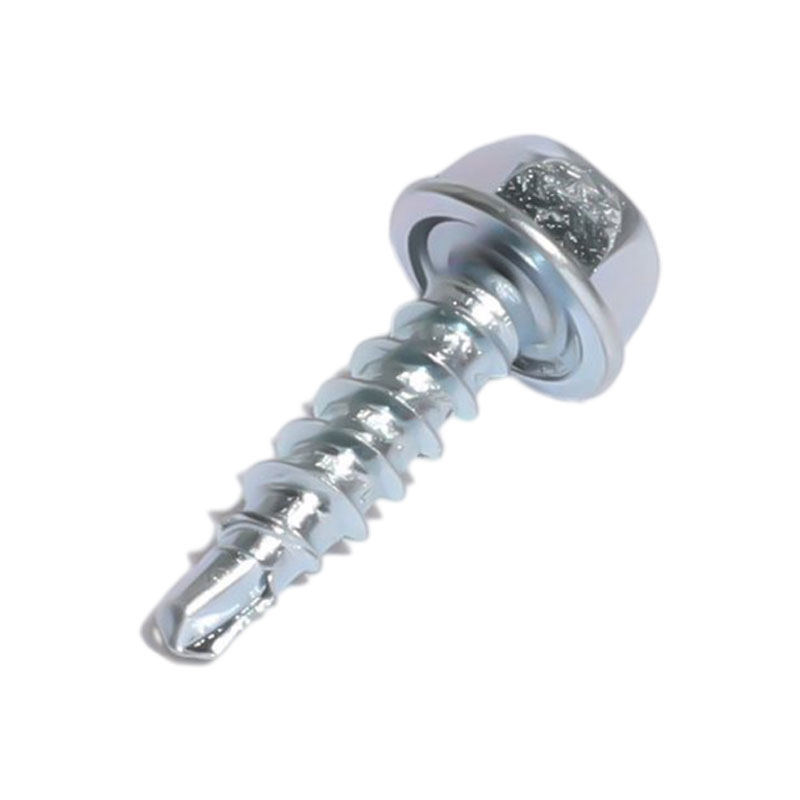
Well designed hex head screws with washer self drilling screws zinc plated
Self-Drilling Performance and Installation Efficiency
A self-drilling screw has a drill-shaped point that cuts through the receiving material as the fastener advances. In many applications, this eliminates the separate drilling and fastening stages associated with ordinary screws. The installer can position the screw and drive it directly through the intended material, provided that the material thickness and screw design are within the fastener’s working range.
This direct installation method can improve productivity in metal framing, sheet metal work, equipment assembly, ductwork, roofing support work, agricultural structures, and general repair tasks. Fewer operations mean fewer tool changes and less opportunity for hole misalignment. In factory assembly, the reduction in handling steps can contribute to a more consistent production rhythm.
The drilling point must be manufactured with accurate geometry. If the point is too blunt, the screw may require excessive pressure and generate unnecessary heat. If the point is inconsistent, drilling time and breakthrough behavior may vary from one screw to another. A well-controlled forming and pointing process helps ensure that the screw begins cutting effectively and maintains a stable path through the material.
Self-drilling performance is affected by several factors, including steel hardness, material thickness, drill-point geometry, driver speed, applied pressure, and the condition of the power tool. Therefore, a screw should not be judged only by its nominal diameter. The complete design, including the point, thread, head, and heat-treatment condition, determines how it behaves in actual use.
When fastening two or more metal sheets, the screw must drill through the upper material and engage sufficiently with the lower material. The selected length should provide adequate thread engagement without leaving excessive projection. Buyers should confirm the combined material thickness and any clearance requirements before placing a large order.
BSD and CSD Thread Options
The product range includes BSD thread and CSD thread configurations. These thread choices are used in self-drilling screw production to support different material and application requirements. The appropriate thread form can influence drilling behavior, chip removal, holding power, and installation speed.
Fine thread configurations are often considered for thinner metal components, while other thread forms may be chosen when a different balance of penetration and engagement is needed. The correct selection depends on the substrate, the thickness of the connected materials, and the required resistance to pull-out or vibration.
Because application conditions vary, professional buyers should communicate the intended material, thickness, tool type, and performance expectations to the supplier. This enables the production team to recommend a suitable diameter, point, thread, head, and coating combination rather than supplying a generic screw for every situation.
Material Selection: C1022A Carbon Steel
C1022A is a widely used carbon steel grade for screw manufacturing. It offers a practical combination of strength, cold-forming suitability, machinability, and availability. These characteristics make it suitable for producing screw blanks, heads, threads, and drilling points through controlled cold heading, rolling, pointing, and related processes.
For a self-drilling screw, the material must support both forming and functional performance. The blank must be sufficiently workable during heading and thread production, while the finished screw must have the hardness and toughness needed to penetrate the intended material without premature failure. Process control is therefore important at every stage.
Material selection alone does not determine screw quality. The final performance also depends on raw material consistency, forming accuracy, heat-treatment control, thread profile, point geometry, surface preparation, and inspection. A competent manufacturer manages these elements as a connected production system.
C1022A is commonly selected for general-purpose fasteners because it can be processed efficiently in large quantities. For applications involving unusual loads, severe corrosion, extreme temperatures, or specialized engineering requirements, the buyer should request a technical review to determine whether the standard carbon steel design is appropriate.
Manufacturing Process and Production Strengths
The manufacturing of a reliable self-drilling screw begins with controlled material preparation. Steel wire or rod suitable for C1022A fastener production is selected according to the required diameter and forming process. Incoming material may be checked for dimensions, surface condition, and basic documentation before it enters production.
Wire Preparation and Cutting
The raw wire is prepared and cut into slugs of controlled length. Accurate cutting is important because the slug volume determines the amount of material available for head formation and shaft development. Variation at this stage can affect head dimensions, overall length, and the transition between the head and shank.
Proper lubrication and tooling preparation help reduce friction during forming. They also support longer die life and more stable production. A clean and well-prepared wire surface contributes to consistent forming and helps reduce defects that could later affect plating adhesion.
Cold Heading and Head Formation
In cold heading, the prepared wire blank is formed under pressure to create the screw head. For a hex washer head design, the forming operation must produce an accurate six-sided profile together with the integrated washer flange. The head must be sufficiently defined for socket engagement while maintaining a smooth transition to the shank.
The washer flange requires particular attention because its diameter, thickness, and underside shape influence bearing performance. An uneven or incomplete flange can create unstable contact with the workpiece. Accurate dies and properly maintained heading equipment help control these dimensions during high-volume production.
Other head styles, such as pan head, flat head, wafer head, bugle head, and pan framing head, require different tooling profiles. The ability to support several head designs demonstrates the flexibility of the production program and allows customers to choose a fastener that matches the assembly appearance and functional needs.
Thread Rolling
Thread rolling forms the screw thread by displacing material rather than cutting it away. This process can produce a strong and continuous thread profile when the blank diameter, tooling, and rolling pressure are correctly matched. It also supports efficient high-volume production and consistent thread dimensions.
For self-drilling screws, the thread must work effectively after the point has penetrated the metal. The thread profile should provide stable engagement and help draw the screw forward while maintaining the connected materials in contact. Thread rolling accuracy contributes to reliable driving behavior and repeatable holding performance.
Thread inspection may include checks of pitch, major diameter, thread form, and gauge acceptance. These controls help prevent assembly problems such as poor engagement, excessive driving resistance, or loose fit with mating components.
Drill-Point Formation
The drill point is a defining component of a self-drilling screw. It is formed to cut the material and establish the initial hole before the thread enters. Point length, cutting edges, symmetry, and tip condition all influence installation performance.
A consistent point helps each screw begin drilling in a predictable way. It can also reduce wandering when the fastener is positioned on a smooth metal surface. Point production must be coordinated with the screw diameter and intended material range. A point suitable for thin sheet may not be appropriate for heavier metal sections.
Production personnel should monitor point shape and ensure that tooling wear does not gradually change the drilling profile. Regular inspection and timely tooling replacement are important for maintaining consistency throughout a production run.
Heat Treatment and Hardness Control
Self-drilling screws require a carefully controlled balance of hardness and toughness. The point must be hard enough to penetrate the material, while the shaft and head must resist twisting or fracture during installation. Heat treatment is therefore a critical step when the application demands reliable drilling performance.
Excessive hardness may make a screw brittle, while insufficient hardness may cause the point to deform before drilling is complete. A controlled thermal process helps create the required mechanical balance. Depending on the production specification, inspections may include hardness testing, torque evaluation, and functional drilling trials.
Manufacturers should also control the transition between heat treatment and surface finishing. Improper cleaning, handling, or thermal exposure can influence coating adhesion and appearance. Coordinated process management helps protect both mechanical performance and corrosion resistance.
Surface Preparation and Plating
The zinc-plated version is designed to provide a bright metallic appearance and a basic level of protection against atmospheric corrosion. Before plating, the screw surface must be cleaned to remove oil, scale, residues, and other contaminants. A clean surface improves the consistency of the zinc coating.
Zinc plating works by placing a protective zinc layer over the steel substrate. Zinc can provide barrier protection and, under suitable conditions, sacrificial protection to exposed steel. However, no standard coating should be considered permanently corrosion-proof. The final service life depends on humidity, salt exposure, temperature, pollutants, contact with dissimilar metals, and installation damage.
Other surface options in the production range include yellow zinc plating, black phosphate, Ruspert, and Magni finishes. These coatings offer different combinations of appearance, corrosion resistance, friction behavior, and application suitability. A buyer should select the finish according to the actual environment rather than choosing only by color.
Coating thickness, adhesion, coverage, and post-treatment are important quality considerations. Areas around the head, thread, and drilling point should receive appropriate coverage without creating excessive buildup that interferes with installation. Coating specifications should be confirmed when the screws are intended for demanding outdoor or industrial environments.
Advantages Compared with Common Alternative Fasteners
Compared with Ordinary Sheet Metal Screws
Ordinary sheet metal screws generally require a pre-drilled hole when they do not have a drilling point. This adds a separate operation and may require a pilot drill of the correct size. A self-drilling screw combines hole creation and fastening, which can reduce installation time and simplify work at height or in restricted spaces.
Pre-drilling can still be appropriate for thick, hard, or delicate materials, and users must not assume that every self-drilling screw can replace every conventional screw. However, where the material thickness falls within the screw’s intended range, the integrated drill point provides a meaningful productivity advantage.
Compared with Separate Bolts and Washers
A bolt-and-washer assembly may provide excellent strength in applications where a prepared through-hole and access to both sides are available. It may be less convenient when only one side of the assembly can be reached. A self-drilling screw can often be installed from one side, reducing labor and eliminating the need to hold a loose nut or washer.
The integrated washer head also reduces component count. This can simplify packaging and decrease the possibility of missing washers during assembly. For high-volume work, fewer components can support more efficient material handling and inventory management.
Compared with Screws Using a Small Recessed Head
A recessed head can provide a clean appearance, but the available driving area may be limited. The hex washer head offers a prominent external driving profile that can be useful for high-speed power-tool installation. It also gives the installer a clear visual indication of the tool interface.
The preferred head style depends on appearance, clearance, access, and torque requirements. The advantage of a product range with multiple head options is that users can choose the most appropriate design rather than compromising on every project.
Compared with Low-Consistency Fasteners
Fasteners with inconsistent point geometry, head dimensions, coating, or thread form can create installation variation. Some may drill easily while others require excessive pressure. Some may seat correctly while others leave an uneven flange or damaged coating. A controlled manufacturing program helps reduce these differences.
Consistency is particularly important for distributors and original equipment manufacturers. Their customers expect the same product to perform similarly across different cartons and production batches. Stable raw materials, maintained tooling, process inspection, and clear specifications all contribute to this expectation.
Surface Finish Selection
Zinc plating is a practical choice for many indoor and moderately protected applications. It offers a familiar appearance and can help slow corrosion under normal atmospheric conditions. It is often selected for general hardware, furniture components, light fabrication, equipment assembly, and construction work where exposure is not severe.
Yellow zinc plating may be selected when a colored passivation appearance or a different corrosion-performance requirement is desired. Black phosphate can provide a dark appearance and useful surface characteristics in selected indoor applications. Ruspert and Magni finishes may be considered for applications requiring enhanced corrosion protection or specific friction and coating performance.
Coating selection must account for installation. Driving the screw can scratch or deform the coating around the head and point. Excessive torque may also damage the surface or deform the washer flange. For outdoor, coastal, chemical, or high-humidity locations, the buyer should define the required corrosion test method, coating thickness, and service expectations before production.
Contact between zinc-plated steel and other metals should also be considered. Dissimilar-metal contact in a wet environment can increase galvanic corrosion risk. Suitable design separation, compatible materials, drainage, and protective coatings may be necessary for long-term performance.
Applications Across Multiple Industries
Metal Fabrication
Metal workshops can use hex washer head self-drilling screws for joining sheet metal, brackets, light frames, enclosures, panels, and support components. The drill point reduces the need for separate pilot-hole preparation, while the washer head provides a broad bearing surface.
Construction and Building Work
Self-drilling screws are used in selected construction tasks involving metal framing, light-gauge steel, interior systems, and accessory installation. The installer should verify the screw’s approved use, material thickness range, required corrosion resistance, and load expectations before application.
Roofing and Exterior Components
Self-drilling screw designs are commonly associated with roofing and exterior sheet applications. The surface finish and sealing arrangement become especially important in these environments. Where water tightness is required, the fastener may need to be used with a suitable sealing washer or system specified for the roofing material. The standard integrated washer head alone should not automatically be treated as a weather seal.
Furniture and Home Tools
In furniture and home tool production, screw selection is influenced by appearance, assembly speed, holding performance, and access to the work area. Different head and recess options can support automated or manual installation. Zinc-plated finishes may be suitable for indoor products where a bright and clean appearance is required.
Packaging and General Hardware
Packaging equipment, storage fixtures, display structures, and general hardware products often require quick joining of metal parts. A self-drilling screw can reduce assembly steps and support repair or maintenance work. Buyers should still confirm that the fastener’s holding capacity is suitable for vibration, repeated loading, and the weight of the assembled components.
Stamping Parts and Metal Hooks
Stamped metal parts and hooks often include thin sections, formed flanges, or overlapping sheets. The washer head can help distribute clamping pressure across the surface, while the drilling point can simplify attachment during secondary assembly. A trial installation is recommended when the stamped part has a curved surface, hardened edge, or limited clearance.
Installation Recommendations
Before installation, confirm the screw diameter, length, thread type, coating, and head style. Check the combined thickness of the materials and ensure that the drilling point is suitable for the harder or thicker layer. The screw should be long enough to obtain effective engagement but not so long that it creates an obstruction or unnecessary exposure.
Use a driver or socket that fits the hex head correctly. A loose tool can round the head, reduce torque transfer, and damage the surface. The driver should be aligned with the screw axis during installation to reduce side loading and prevent the fastener from wandering.
Apply steady pressure while the drilling point is cutting. Excessive downward force may damage the point or distort thin sheet material. Excessive speed can generate heat and cause premature wear. The best tool speed depends on screw diameter, material thickness, substrate hardness, and equipment type.
Stop tightening when the washer flange is seated firmly against the material. Overdriving can deform the flange, strip the connected material, damage the coating, or reduce the effective clamping force. Underdriving can leave the assembly loose and may allow movement or vibration.
For production lines, installation trials should be conducted using the actual material, tool, speed, and torque settings. A successful trial should evaluate drilling time, seating condition, head damage, material deformation, and holding performance. Standardized settings can then be documented for operators.
Quality Control Considerations
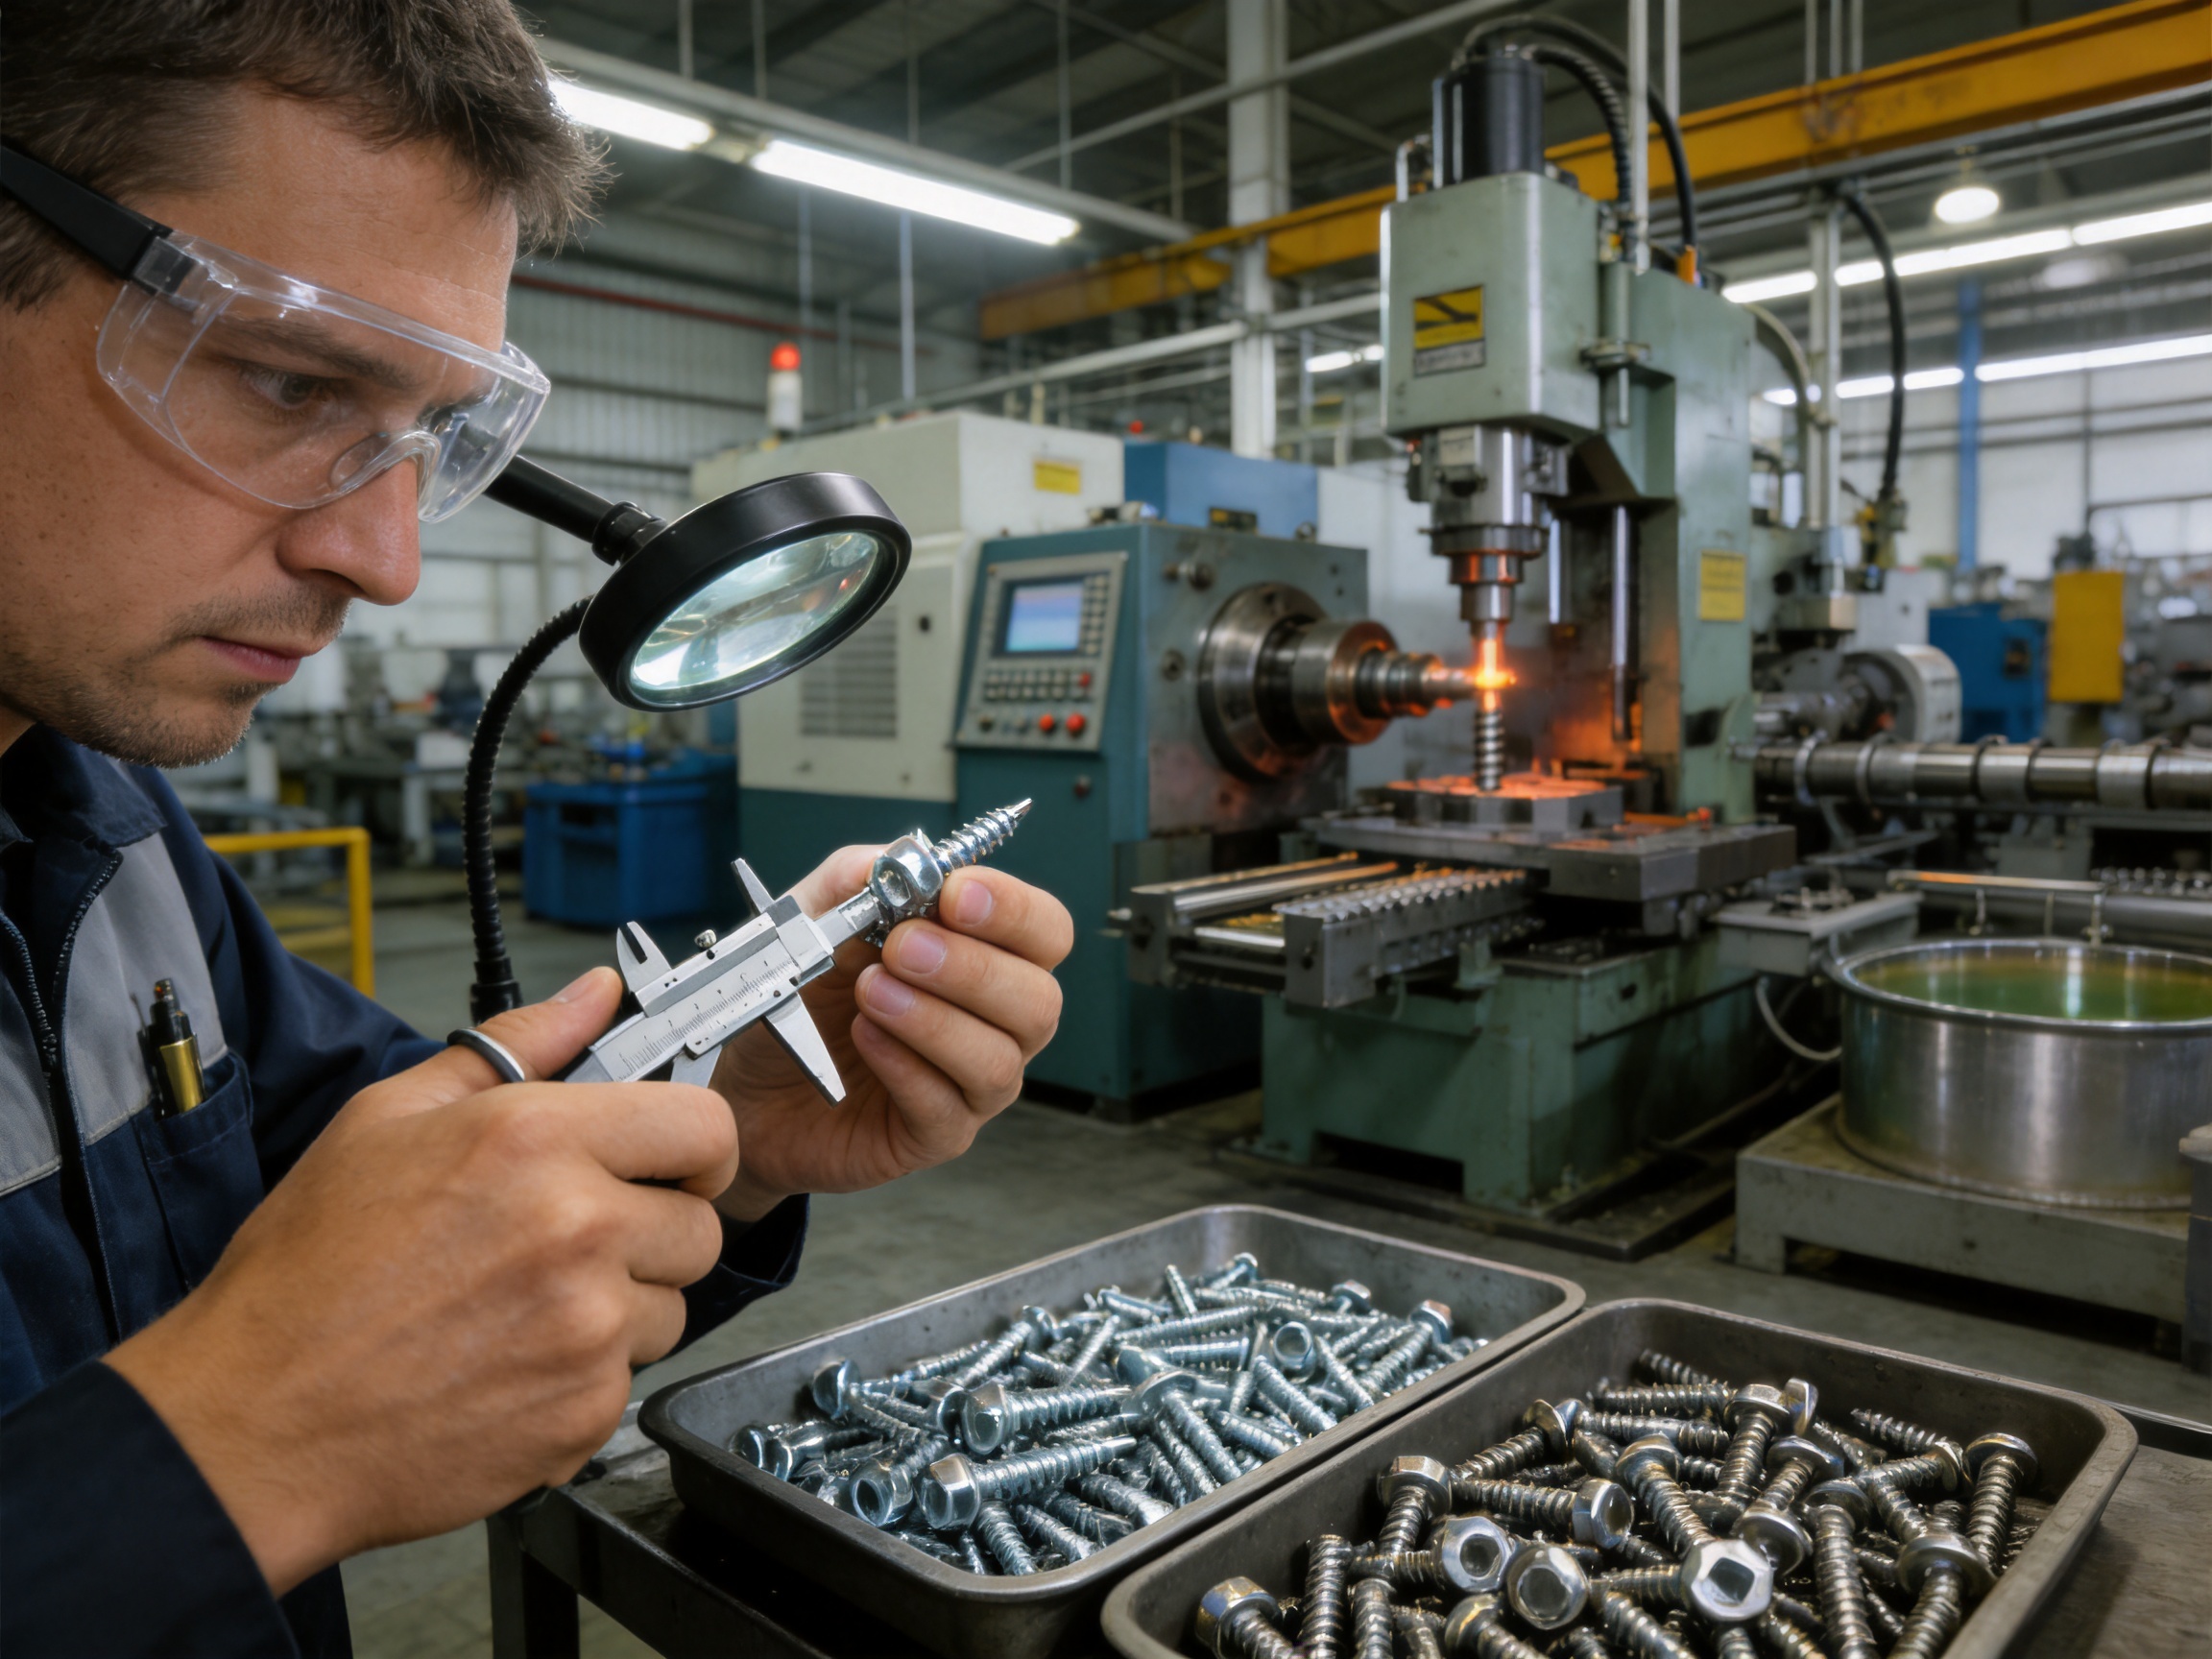
Quality control should begin with incoming raw material and continue through forming, thread rolling, pointing, heat treatment, coating, packaging, and final inspection. A finished screw can look acceptable while still having a hidden issue in hardness, point geometry, coating adhesion, or thread accuracy, so functional testing is valuable.
Dimensional inspection may cover overall length, diameter, head height, washer diameter, head width, thread dimensions, and point geometry. These measurements help ensure compatibility with tools, assembly fixtures, and customer drawings.
Visual inspection can identify burrs, cracks, incomplete heads, damaged threads, uneven plating, stains, and surface contamination. Although visual checks do not replace mechanical testing, they are an important part of batch release and packaging control.
Mechanical and functional evaluations may include hardness testing, torsional testing, pull-out testing, drive testing, and drilling trials. The specific tests should be selected according to the customer’s specification and intended application. For products sold under recognized standards, the applicable requirements should be reviewed carefully rather than relying on a general description.
Packaging inspection is also significant. Screws should be counted or weighed using a controlled method, packed to prevent excessive rubbing, and labeled with the correct diameter, length, head type, finish, thread, quantity, and batch information. Clear packaging helps distributors avoid mixing similar products in warehouses.
Manufacturing and Supply Advantages
Lizhan Hardware Co., Ltd. provides a production range covering self-drilling screws, drywall screws, sheet metal screws, roofing screws, furniture screws, and related hardware. This product breadth is useful for buyers who need several screw families for one market or project category.
The available production range includes multiple head forms, recess styles, diameters, thread options, and surface treatments. Such flexibility allows the manufacturer to support standard products as well as application-specific requirements. It also gives customers more opportunities to coordinate appearance and function across a product line.
The company operates a China factory and maintains a Thailand warehouse location. A manufacturing base in China supports production and sourcing, while an additional warehouse presence can assist regional distribution and stock planning for customers in relevant markets. Buyers should confirm current inventory, shipping arrangements, minimum order quantities, and lead times for each item.
The company’s production strengths are most relevant when they are connected to measurable requirements. Customers may request drawings, samples, material information, coating details, packaging specifications, inspection procedures, and batch documentation. This approach helps convert a general product inquiry into a clear and verifiable purchasing specification.
For distributors, the ability to purchase related fasteners from one supplier may reduce supplier management work. For manufacturers, product customization can help align screw dimensions and finishes with an existing assembly process. For contractors, consistent supply of common sizes can simplify field inventory and reduce the need to substitute products at the job site.
Customization and Procurement Support
Although the listed product is a standard zinc-plated hex washer head self-drilling screw, many commercial buyers require specific packaging, labeling, dimensions, or surface treatments. These requirements should be defined before quotation and confirmed on the purchase order.
Important inquiry details include nominal diameter, length, head type, thread configuration, point type, material, finish, quantity, packaging format, and required standard. A drawing or reference sample is helpful when the buyer needs a non-standard profile or a special washer dimension.
Packaging may include bulk cartons, small boxes, plastic containers, retail cards, or customized labels. The correct format depends on whether the product is sold to industrial users, hardware distributors, retailers, or project contractors. Labels should clearly identify the product to prevent mixing during storage and installation.
For recurring orders, buyers should establish an approved sample and a documented specification. Subsequent batches can then be checked against the approved reference. This is particularly useful when the product is supplied under a private label or distributed across several markets.
Environmental and Corrosion Considerations
Fastener selection should reflect the environment in which the screw will be used. Indoor dry conditions are generally less demanding than outdoor, coastal, industrial, agricultural, or chemically exposed locations. Zinc plating may be adequate in some environments but insufficient in others.
Humidity, salt spray, condensation, fertilizers, cleaning chemicals, and industrial pollutants can accelerate corrosion. Even a well-coated screw may have reduced life if the coating is scratched, the fastener is overdriven, or water is trapped around the joint.
Designers should consider drainage, joint movement, exposure, maintenance access, and contact with other metals. Where corrosion resistance is critical, the buyer should request coating test information and select a finish based on a defined performance requirement rather than a general color description.
Responsible production also benefits from efficient material use, process control, and reduced rejection rates. Accurate forming and inspection help limit waste by identifying problems early. Buyers may request information about packaging efficiency and production quality practices when environmental performance is part of their procurement policy.
Why Product Consistency Matters to Competitors and Buyers
In a competitive fastener market, price is only one part of total cost. A screw that is slightly cheaper but causes frequent point failures, damaged heads, installation delays, or customer complaints may create a higher overall cost. Consistency can therefore be a more valuable advantage than a low unit price alone.
A stable self-drilling screw should deliver reasonably uniform drilling time, driving resistance, head seating, and coating appearance from batch to batch. This helps contractors estimate labor, helps factories maintain production settings, and helps distributors reduce returns.
The combination of a functional hex washer head, integrated flange, self-drilling point, C1022A material, and available surface treatments gives this product a balanced position against competing fasteners. Its strongest advantage is not a single feature but the way several features work together to reduce installation steps and support practical metal assembly.
Customers comparing suppliers should evaluate samples under real conditions. Testing should use the actual sheet material, tool, speed, and installation method. A supplier that can discuss the relationship between material, point geometry, thread, coating, and application is better positioned to provide a suitable product than one that offers only a nominal size list.
Frequently Asked Questions
What is a hex washer head self-drilling screw?
It is a fastener with a six-sided external head, an integrated washer flange, and a drill-shaped point. The point can create a hole in suitable metal material while the thread advances into the workpiece. The integrated flange helps distribute clamping pressure beneath the head.
Does the screw always eliminate pre-drilling?
No. It can eliminate pre-drilling when the material thickness and hardness are within the screw’s intended working range. Very thick, hardened, brittle, or delicate materials may still require a pilot hole or a different fastening method.
What material is used for this product?
The listed product is made from C1022A carbon steel. This grade is widely used for screw production because it supports forming and can provide suitable mechanical performance when processed and heat-treated correctly.
What diameters are available?
The listed diameter range includes #6-3.5, #8-4.2, #10-4.8, #12-5.5, and #14-6.3. The most suitable size depends on material thickness, required holding power, clearance, and the selected application.
Which head styles are available in the production range?
Available head options include hex washer head, bugle head, flat head, pan head, wafer head, and pan framing head. The hex washer head is the focus of this article, but the wider range allows buyers to select a different profile when appearance or assembly conditions require it.
Which driving recesses can be supplied?
The listed recess options are Phillips, square, and Torx. The correct recess depends on the driver system, required torque transmission, automation equipment, and customer preference.
What finishes are available?
The production range includes zinc plated, yellow zinc plated, black phosphate, Ruspert, and Magni finishes. Finish selection should be based on corrosion exposure, appearance, friction requirements, and the customer’s technical specification.
Is zinc plating suitable for outdoor use?
Zinc plating may be suitable for some protected or moderately exposed outdoor applications, but suitability depends on the environment and required service life. Coastal, high-humidity, chemical, or heavily exposed conditions may require a more resistant coating system.
What are BSD and CSD threads?
BSD and CSD are thread configurations used in self-drilling screw production. They are selected according to the substrate, thickness, drilling behavior, and required engagement. Buyers should specify the material and application so the appropriate thread can be recommended.
How should the screw be installed?
Use a correctly fitted socket or driver, align the tool with the screw, apply steady pressure while drilling, and stop when the washer flange is firmly seated. Avoid excessive torque because overdriving can damage the coating, flange, material, or thread engagement.
Can the product be customized?
Customization may be possible for dimensions, head styles, recesses, threads, finishes, packaging, labels, and other commercial requirements. Buyers should provide a drawing, sample, or detailed specification for review before production.
What information should be included in a quotation request?
A quotation request should include diameter, length, head type, thread type, point type, material, finish, quantity, packaging, required standard, destination, and application. Samples or drawings are recommended for non-standard products.
Why is C1022A commonly used for screws?
C1022A offers a practical combination of formability and strength for many general-purpose screw designs. Its final performance still depends on the forming process, heat treatment, thread quality, point geometry, and inspection controls.
Are these screws suitable for structural applications?
They may be suitable for selected light-duty or non-critical metal fastening tasks, but users should not assume that a general self-drilling screw is a structural fastener. Structural applications require a verified design, suitable standards, calculated loads, and confirmation of the fastener’s mechanical performance.
How can buyers compare competing suppliers?
Buyers should compare samples, dimensional consistency, drilling performance, coating quality, packaging accuracy, documentation, production capacity, lead time, and after-sales support. The lowest purchase price does not always represent the lowest total cost.
Conclusion
Well-designed hex washer head self-drilling screws provide a practical solution for joining suitable metal materials quickly and efficiently. Their integrated drill point reduces installation steps, their hexagonal head supports positive tool engagement, and their washer flange helps distribute clamping pressure across the surface.
The product range is strengthened by the use of C1022A carbon steel, multiple diameters, BSD and CSD thread options, several head styles, Phillips, square, and Torx recesses, and a selection of zinc-based and specialty surface treatments. This flexibility enables the fastener to serve metal fabrication, construction, furniture, packaging, home tool, roofing, stamping, and general hardware markets.
Reliable performance depends on more than the visible shape of the screw. Raw material quality, cold heading, head formation, thread rolling, point geometry, heat treatment, coating preparation, plating, inspection, and packaging must all be controlled. A manufacturer with a broad production program and the ability to support specification-based purchasing can provide greater value than a supplier offering only a narrow standard range.
For the best result, users should select the screw according to substrate, thickness, environment, load, tool, and installation method. A sample trial using the actual application is recommended before large-scale production or field deployment. When correctly selected and installed, the zinc-plated hex washer head self-drilling screw can deliver a dependable balance of speed, convenience, holding performance, and supply flexibility.
References
ASTM International. Standards and guidance relating to mechanical fasteners, carbon steel materials, dimensional requirements, and corrosion testing.
DIN 7504K. Self-drilling screws with hexagon washer head and related dimensional specifications.
DIN 7504P. Self-drilling screws with countersunk head and related product requirements.
DIN 7504N. Self-drilling screws with pan head and related product requirements.
International Organization for Standardization. General principles for fastener dimensions, mechanical properties, thread systems, and quality inspection.
Fastener engineering manuals covering cold heading, thread rolling, heat treatment, drilling-point formation, and surface finishing.
Technical literature on zinc plating, passivation, corrosion protection, and coating performance for carbon steel fasteners.
Industrial guidelines for screw installation torque, substrate selection, power-tool operation, and inspection of self-drilling fasteners.